


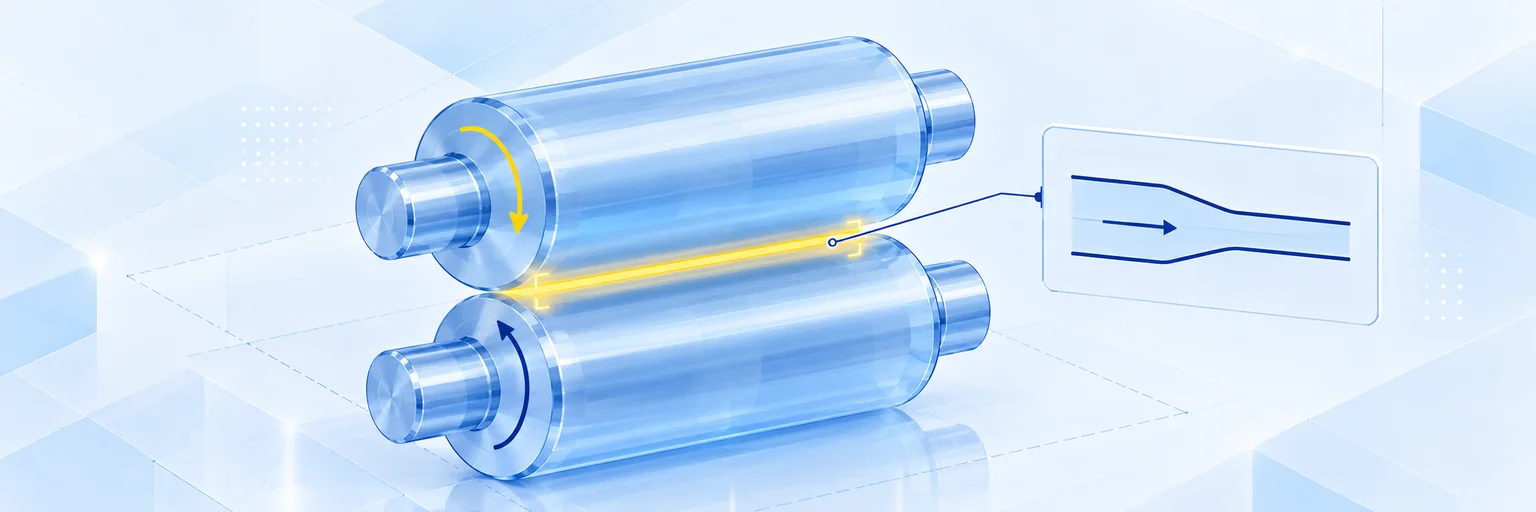
The rolling process shapes metal by passing it between rotating rolls. Instead of producing finished parts, rolling mainly produces the semi-finished materials that almost every other process starts from — sheets, plates, bars and tubes. Its key advantage is the ability to mass-produce uniform metal material quickly and at relatively low cost.
This article explains how rolling works, how hot rolling, cold rolling and warm rolling differ, and which rolling mills are used for which products — plus what this means when you choose material for your custom parts.
What is the rolling process?
In the rolling process, metal is passed through rotating rolls that compress it and stretch it in length. This plastic deformation process is known for producing material with a uniform cross-section at high speed. Rolled products range from metal sheets and plates to bars, rods, long sections and even square or round tubes.
Rolled material is used extensively in construction and manufacturing. Sheet metal produced by rolling, for example, is the starting material for beverage cans, batteries and automotive parts.
Depending on the processing temperature, rolling is divided into three types: hot rolling, cold rolling and warm rolling.
Hot rolling vs. cold rolling vs. warm rolling
The table compares the three types of rolling for steel. The sections below explain each one in detail.
| Property | Hot rolling | Cold rolling | Warm rolling |
|---|---|---|---|
| Temperature (steel) | Approx. 900–1,200 °C | Usually room temperature | Approx. 600–900 °C |
| Relative to recrystallization | Above | Below | Below, but at elevated temperature |
| Forming force | Low | High | Medium |
| Dimensional accuracy | Lower | High | Medium |
| Surface | Mill scale (oxide layer) | Smooth and bright | Better than hot rolling |
| Work hardening | None | Yes — higher strength, lower ductility | Reduced |
| Typical products | Plates, thick sheets, sections, rails | Thin sheets and strip with tight tolerances | Products that are difficult to roll hot or cold |
Hot rolling
In hot rolling, the metal is heated before processing to make it easier to form. For steel, this means temperatures of roughly 900–1,200 °C: the material is red-hot when it passes through the rolls. Because the temperature is above the recrystallization point, the structure of the metal re-forms continuously during rolling.
Advantages
- Better formability: at high temperatures, the metal's resistance to deformation drops, so large reductions are possible with less force.
- Improved material structure: recrystallization refines the grain structure and results in a tough material.
- No work hardening: since the material is processed above its recrystallization temperature, it does not harden during rolling.
Disadvantages
- Lower dimensional accuracy: large temperature changes during and after rolling cause the material to shrink unevenly.
- Surface quality: in contact with air, the hot surface oxidises and forms mill scale, which leaves a rougher, less attractive finish.
- Energy and cost: heating the material requires a lot of energy and increases cost.
Cold rolling
Cold rolling takes place below the recrystallization temperature of the metal — usually at room temperature, without heating the material beforehand. The material still warms up during forming, but it is not heated intentionally. Cold rolling is typically used to roll hot-rolled material down to thin, precise sheet and strip.
Advantages
- No heating equipment required: the material is processed at room temperature and is easier to handle.
- High dimensional accuracy: cold rolling achieves tighter thickness tolerances than hot rolling.
- Attractive finish: the process produces a smooth, bright surface.
- Higher strength: work hardening increases the strength and hardness of the material.
Disadvantages
- High deformation resistance: at low temperatures, the metal resists deformation more strongly, so rolling requires more force.
- Work hardening: the material becomes harder and less ductile. To restore formability, a subsequent heat treatment such as annealing is often needed.
Warm rolling
Warm rolling sits between hot and cold rolling. For steel, it is typically carried out at around 600–900 °C. The process combines some of the benefits of both: it requires less force than cold rolling and achieves better dimensional accuracy and surface quality than hot rolling. Warm rolling is mainly used for materials and products that are difficult to roll hot or cold.
Types of rolling mills
Rolling mills are the machines that carry out the rolling process. Their configuration depends on the desired shape and the number of rolls. The table gives an overview of six common types.
| Rolling mill | Roll arrangement | Typical use |
|---|---|---|
| Two-high mill | Two opposing rolls | Breaking down ingots into slabs, simple flat rolling |
| Four-high mill | Two work rolls, each supported by a backup roll | Precise flat rolling of steel, copper and aluminium |
| Cluster mill | Small work rolls supported by many backup rolls | Hard metals such as stainless steel, very thin foil |
| Planetary mill | Many small work rolls around a large backup roll | Very large reductions in a single pass |
| Universal mill | Horizontal and vertical rolls | Sections such as H-beams |
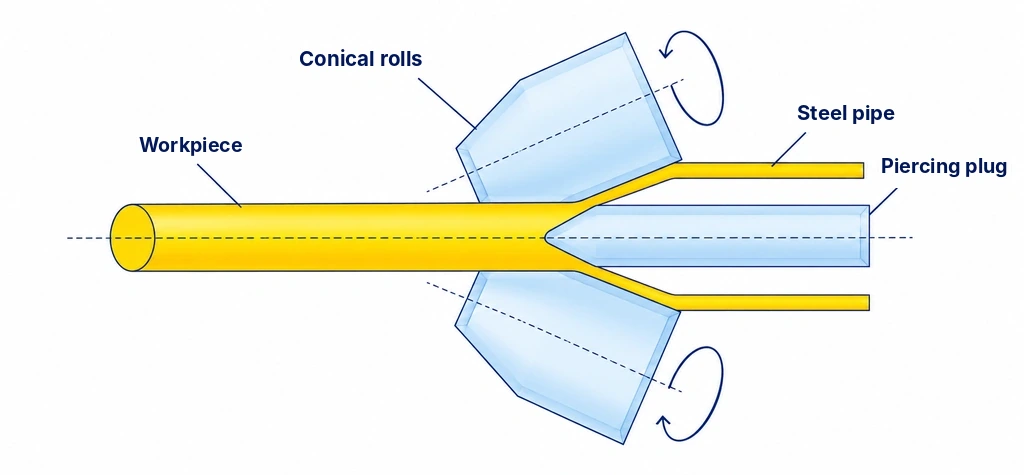
| Piercing mill (Mannesmann) | Skewed conical rolls and a piercing plug | Seamless steel tubes |
Two-high rolling mill
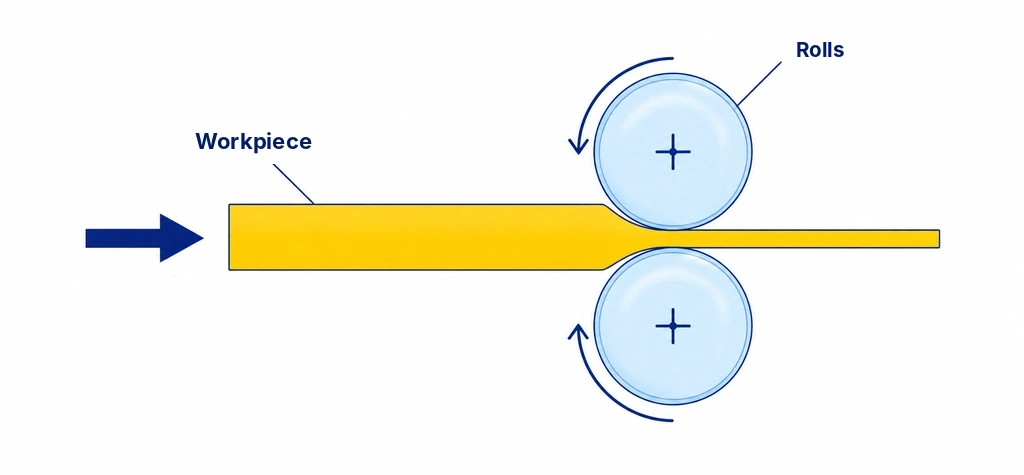
The two-high rolling mill consists of two opposing rolls that compress the metal. This simple design is used for rough rolling — for example, breaking down cast ingots into slabs — as well as for simple flat rolling.
Four-high rolling mill
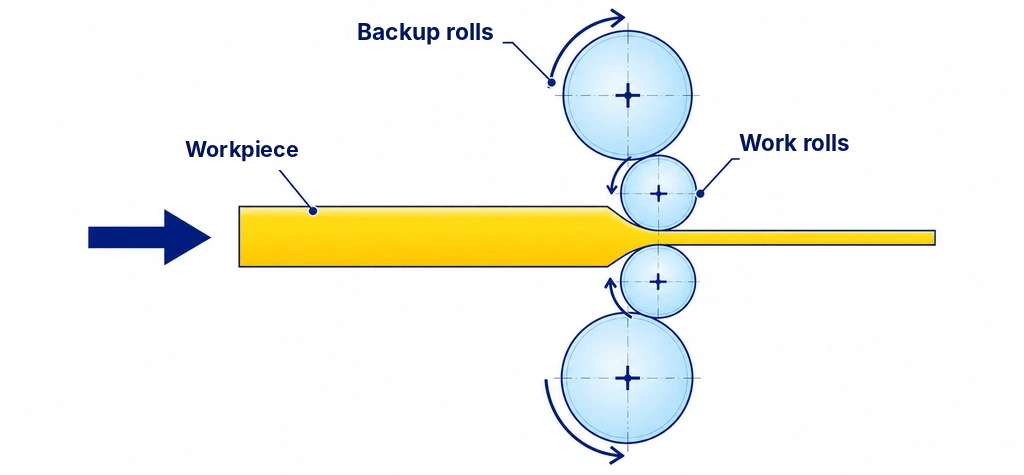
A four-high rolling mill has two work rolls, each supported from behind by a larger backup roll. The backup rolls reduce the deflection of the work rolls, which enables high-precision rolling. Four-high mills are used for steel as well as copper and aluminium.
Cluster mill (multi-roll mill)
Cluster mills, also called multi-roll mills, have even more backup rolls than four-high mills. The name comes from the cluster of backup rolls that support each work roll and allow very high rolling pressure. This makes it possible to roll hard metals such as stainless steel. Thanks to the small work roll diameter and strong support, the work rolls do not deflect, so cluster mills are ideal for cold rolling extremely thin material such as copper foil.
Planetary rolling mill
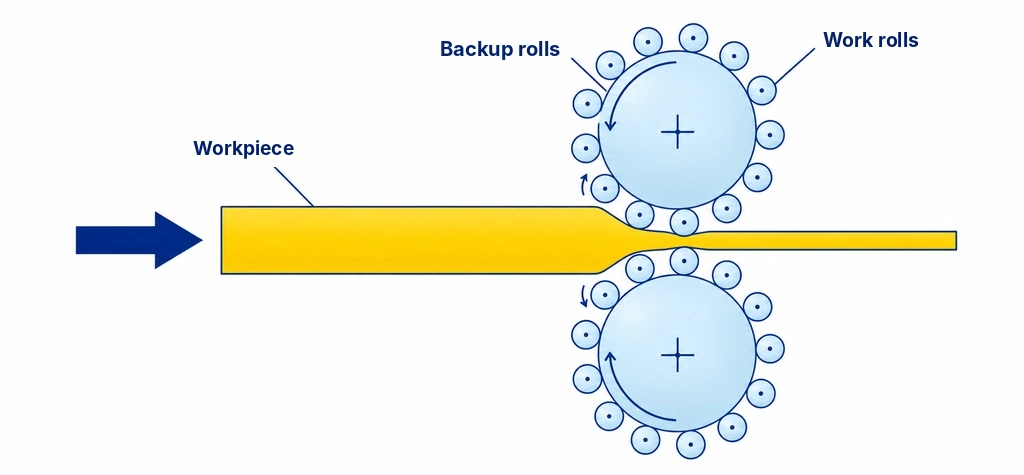
In a planetary rolling mill, many small work rolls are arranged around the circumference of a large backup roll. The small rolls pass over the material in a planetary motion, which allows very large reductions and high rolling efficiency. This design is especially effective for heavy reductions and large material volumes.
Universal rolling mill
Universal rolling mills have both horizontal and vertical rolls, so they can apply pressure from several directions at once. This makes them suitable for rolling complex cross-sections such as H-beams from pre-shaped blooms or beam blanks.
Piercing mill (Mannesmann mill)
Piercing mills, or Mannesmann mills, produce seamless steel tubes. Two skewed, conical rolls rotate a solid round billet and drive it forward over a piercing plug, which forms the hollow shell from the inside. Because the tubes have no weld seam, they are ideal for high-pressure applications such as oil pipelines, boilers and other critical infrastructure that transports liquids or gases.
Rolled materials for parts from meviy
meviy manufactures individually designed custom parts from your own 3D CAD data — not standard or catalogue parts. Most of the materials you can choose are rolled products, and knowing whether a material is hot-rolled or cold-rolled helps you anticipate its surface and accuracy:
- Low-carbon steel sheet EN 1.0330 equiv. (EN 1.0320 equiv. [hot coiled]) from 0.8 to 6.0 mm for parts made by sheet metal fabrication
- Zinc-plated variants EN 1.0330 equiv. (Electrolytic Zinc Plating) and EN 1.0330 equiv. (Galvanized) — see SECC vs. SGCC
- Hot-rolled structural steel EN 1.0038 equiv. for plates from 9 to 16 mm — more on this in our carbon steel guide
- Stainless steel sheet EN 1.4301 equiv. and EN 1.4016 equiv., and aluminium sheet EN AW-5052 equiv.
- Rolled flat bar and plate as starting material for parts made by CNC milling
Sheet metal parts are cut to shape by laser cutting and formed by bending. You upload your 3D model, choose the material and get the price and delivery date instantly.
Frequently asked questions about the rolling process
What is the difference between hot-rolled and cold-rolled steel?
Hot-rolled steel is rolled above its recrystallization temperature. It is easier to form but has lower dimensional accuracy and a scaled surface. Cold-rolled steel is rolled at room temperature: it has tighter tolerances, a smooth surface and higher strength due to work hardening, but it costs more to produce.
Is cold-rolled steel stronger than hot-rolled steel?
Generally yes. Cold rolling hardens the material, which increases its strength and hardness but reduces ductility. If the material needs to be formed further, it is often annealed after cold rolling to restore its formability.
What do SPCC and SPHC mean?
SPCC and SPHC are Japanese JIS designations for cold-rolled and hot-rolled low-carbon steel sheet. At meviy Europe, the corresponding sheet material is listed as EN 1.0330 equiv., with the hot-coiled variant EN 1.0320 equiv.
What is a four-high rolling mill used for?
A four-high mill uses two small work rolls supported by two larger backup rolls. The backup rolls prevent the work rolls from deflecting, so the mill can roll sheet and strip of steel, copper or aluminium with high thickness accuracy.
Rolling: the basis for sheet, bar and tube
Rolling is a plastic deformation process in which metal is passed through rolls to produce sheets, bars or tubes. Depending on the temperature, it is divided into hot rolling, cold rolling and warm rolling. The rolling mills vary with the application: two-high, four-high and cluster mills are common for flat products, universal mills produce sections such as H-beams, and piercing mills make seamless tubes. Knowing how your material was rolled helps you choose the right sheet or bar for your parts.